Chemical pumps play an essential role in numerous industries. They facilitate the secure and efficient transfer mixing and dispensing of chemicals. These pumps are designed to handle fluids which cannot be handled by traditional pumps. Chemical pumps are divided into two types which are centrifugal pumps, and positive displacement pumps.
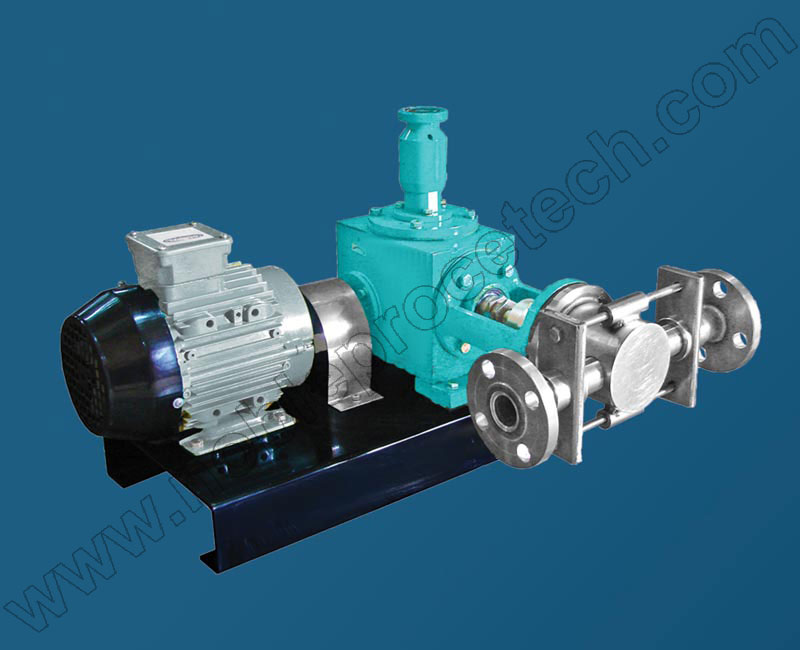
By partnering with reputable chemical pumps manufacturers and suppliers, you will have access to premium chemicals that meet the standards of the industry. These companies make use of their expertise to develop chemical pumps that are durable, durable, efficient, and cost-effective. These companies make use of the latest techniques and materials to design pumps that can stand up to the extreme chemical. By working with trusted manufacturers firms can have access to pumps that are designed to endure harsh conditions and work optimally.
Chemical transfer pumps have been designed specifically for fluid transfer. They are capable of handling diverse chemicals, including acetic and sulphuric acids such as sodium hypochlorite and. Chemical transfer pumps are manufactured by companies that focus on efficient control of fluids. These include features like corrosion resistant materials, leak-proof seals with precise flow control devices as well as other features. The pumps are designed to assure smooth, safe and accurate chemical transfer.
Chemical pump suppliers are crucial in helping businesses find the best pumps that meet their needs. They offer a broad variety of chemical pumps from trusted manufacturers. They offer extensive product catalogs, technical support as well as customer service to assist companies in choosing the correct pumps for specific requirements. Chemical pumps suppliers make sure that companies have access various options, and are able to find the ideal solution to their business needs.
The importance of dependable chemical pumps goes beyond protecting fluids. They are critical to maintaining the integrity and safety of an whole industrial process. Pumps that are not reliable or has a malfunction can lead to expensive leaks, low performance, and even hazards. Pump failure can have severe consequences for industries that use chemicals, for example chemical manufacturing and the use of petrochemicals. For more information, click chemical manufacturing pump
By investing in reliable chemical pumps, businesses can lessen the risks related to handling fluids. They’re designed and constructed to withstand the corrosive qualities of different chemicals, so that they function reliably and effectively over the course of time. They’re equipped with features like robust material, advanced sealing mechanisms, and precise flow control all of which are essential to the secure and reliable transfer of fluids.
Furthermore, reliable chemical pumps typically come with complete maintenance and support. The manufacturers and suppliers are aware of the importance of chemical pumps and provide technical assistance, spare parts availability, and maintenance inspections. This proactive approach allows the detection and resolution of any potential problems prior to them becoming serious. This ensures long-term pump efficiency and helps reduce unexpected downtime.
Chemical pumps can be used in many industries, such as food processing, chemical manufacturing and petroleum chemicals. These industries serve as vital components for fluid flow mixing and dispensing. Chemical pumps can also be found in high-temperature systems for heating and in refineries. Their capacity and flexibility to handle challenging fluids make them vital tools in ensuring efficient and reliable industrial processes.
When choosing a chemical pumps it is essential to think about factors like the type of fluid being used, the flow requirements, operating conditions as well as compatibility with chemicals. A reputable chemical pump manufacturer and suppliers provide guidance and help in choosing the right pump for specific applications. The importance of safety, efficiency, and reliability is essential when selecting a chemical pumps to prevent potential dangers, optimize productivity and minimize downtime.
Chemical pumps are utilized in a variety of ways that go far beyond the refinery. They can be used for a variety of purposes and play a crucial part in the transportation of chemicals off-site. Chemical pumps play an essential function in the smooth operation of refineries outside their boundaries. They can transport liquids that are corrosive, load and unload tanker truck or aid in maintenance and repair. Chemical pumps are necessary for applications that require precision, safety, as well as effectiveness when dealing with corrosive and abrasive chemical substances. With the assistance of reliable chemical pump manufacturers and suppliers and by investing in high-quality pumps refineries can keep a solid foundation for their operations off-site and ensure dependable chemical transfer.